
Problem: recurring gaps between designs and scalable output
Brands commission a new silhouette, expect a straight path to production, and then face surprises: material substitutions, assembly bottlenecks, unexpected tooling costs and inconsistent fit across batches. Designers will ask for a modular backpack and expect prototypes to translate directly into a 10,000-unit order. That expectation creates financial strain when suppliers lack repeatable processes or clear cost models.

Why these gaps appear
Three operational faults recur. First, specification ambiguity—drawings that omit tolerances or seam allowances lead to rework. Second, supplier fragmentation—separate cutters, stitchers and hardware vendors operate on misaligned lead times. Third, testing omission—no defined mechanical or wear tests means defects surface only after distribution. Each fault drives overruns, erodes margins, and risks brand reputation.
Technical controls that close the loop
Apply measurable controls at four points. Lock tolerances and constructible drawings before tooling. Quantify material substitutions with cost-per-piece models so changes map to margin impact. Institute staged pilot runs: 50 units, then 500, then full scale, each with prespecified defect-rate thresholds. Adopt a component master file that tracks supplier lot, dye lot, and hardware torque specs. Use clear acceptance criteria for stitches per inch, seam strength (N/mm) and zipper pull cycles.
Experience and authoritative proof points
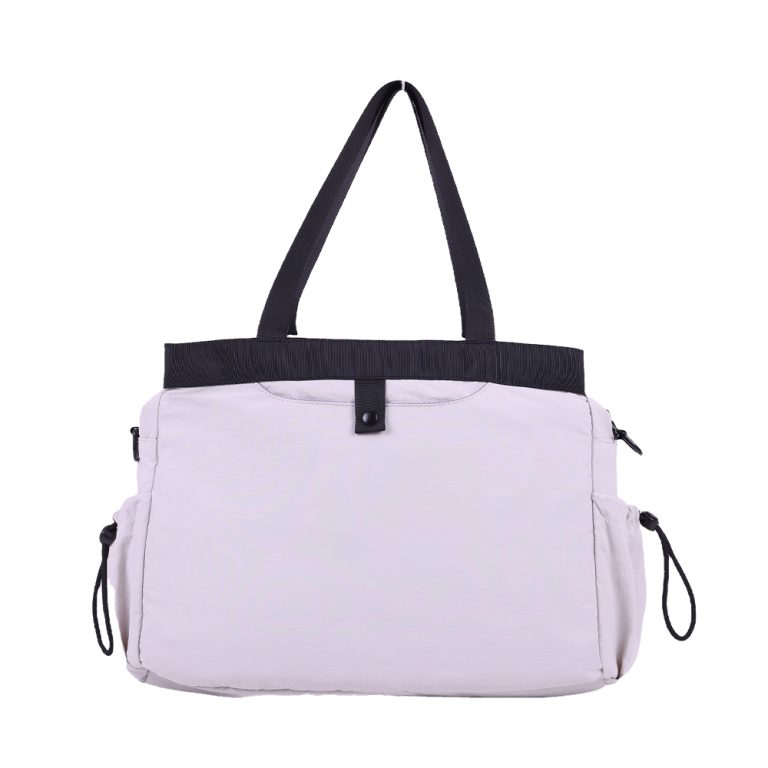
I’ve led factory audits and production ramp reviews across Asia for over a decade, running structured line-balance tests and root-cause analyses that reduced first-pass defects by measurable margins. Industry showcases confirm practical demand: prototypes of expandable carry systems gained notice at CES 2023, illustrating market interest and technical feasibility. For a concrete product example and specification baseline, see Expandable Backpack, which demonstrates modular compartments and validated hardware details used in production assessment.
Quality assurance, compliance and measurable KPIs
Define four KPIs and enforce them at every handoff: incoming material acceptance rate, pilot defect rate, assembly throughput (pieces per operator-hour), and field return rate within 12 months. Require third-party lab reports for abrasion, water resistance and zipper endurance where claims matter. Use process capability (Cpk) to determine whether a stitch or cut process can hit tolerance consistently; if Cpk < 1.33, redesign the process rather than accepting more inspection.
Common pitfalls that derail production
Relying on sample approval as a production guarantee. Ignoring change control for hardware substitutions. Using price alone to select a lead supplier without a demonstrated ability to scale. Expecting a single line trial to validate a subassembly that will later be outsourced to three separate vendors. Each pitfall creates non-linear cost and time failures.
Implementation checklist for an accountable program
Create a 90-day rollout plan: freeze specs, conduct supplier capability audits, run two staged pilots with documented acceptance criteria, codify a failure-mode-and-effects log, and assign a cross-functional owner with financial authority to approve supplier changes. Tie payment milestones to verified KPIs. Record every deviation and its margin impact to build a decision log for future styles.
Conclusion
A problem-driven approach delivers predictable outcomes: fewer overruns, transparent margins, and repeatable quality. The work is technical and operational—tight tolerances, staged pilots, supplier capability metrics. That disciplined path is what differentiates sample-stage success from profitably scalable production and is the practical value teams find when they engage with partners like ChangRong.






