
Introduction — a quick scene, a few facts, and the question we all avoid
I was on a late shift once, watching a crew swap out a stubborn pump motor while the plant hummed in the background — tools clicking, radios on, everyone trying to keep the job on schedule. In that moment I realized how easily a simple wrench slip could trigger a spark; that’s why we use non sparking sockets in these zones. Recent safety audits show tool-related ignition still ranks high in incident logs (around 12–18% in some facilities), and yet teams often treat safe tools as an afterthought. How do we make safer tool choices feel like part of our standard automation and deployment work instead of an add-on? I want to share practical observations from the floor — automation hooks, checklist changes, and a few process tweaks I’ve seen actually stick — so teams can close the gap between policy and practice. This will guide us into the deeper trade-offs behind tool selection and the hidden problems most managers don’t spot. Let’s unpack that next.
Part 2 — Where the usual fixes fail: a technical look at non sparking impact sockets
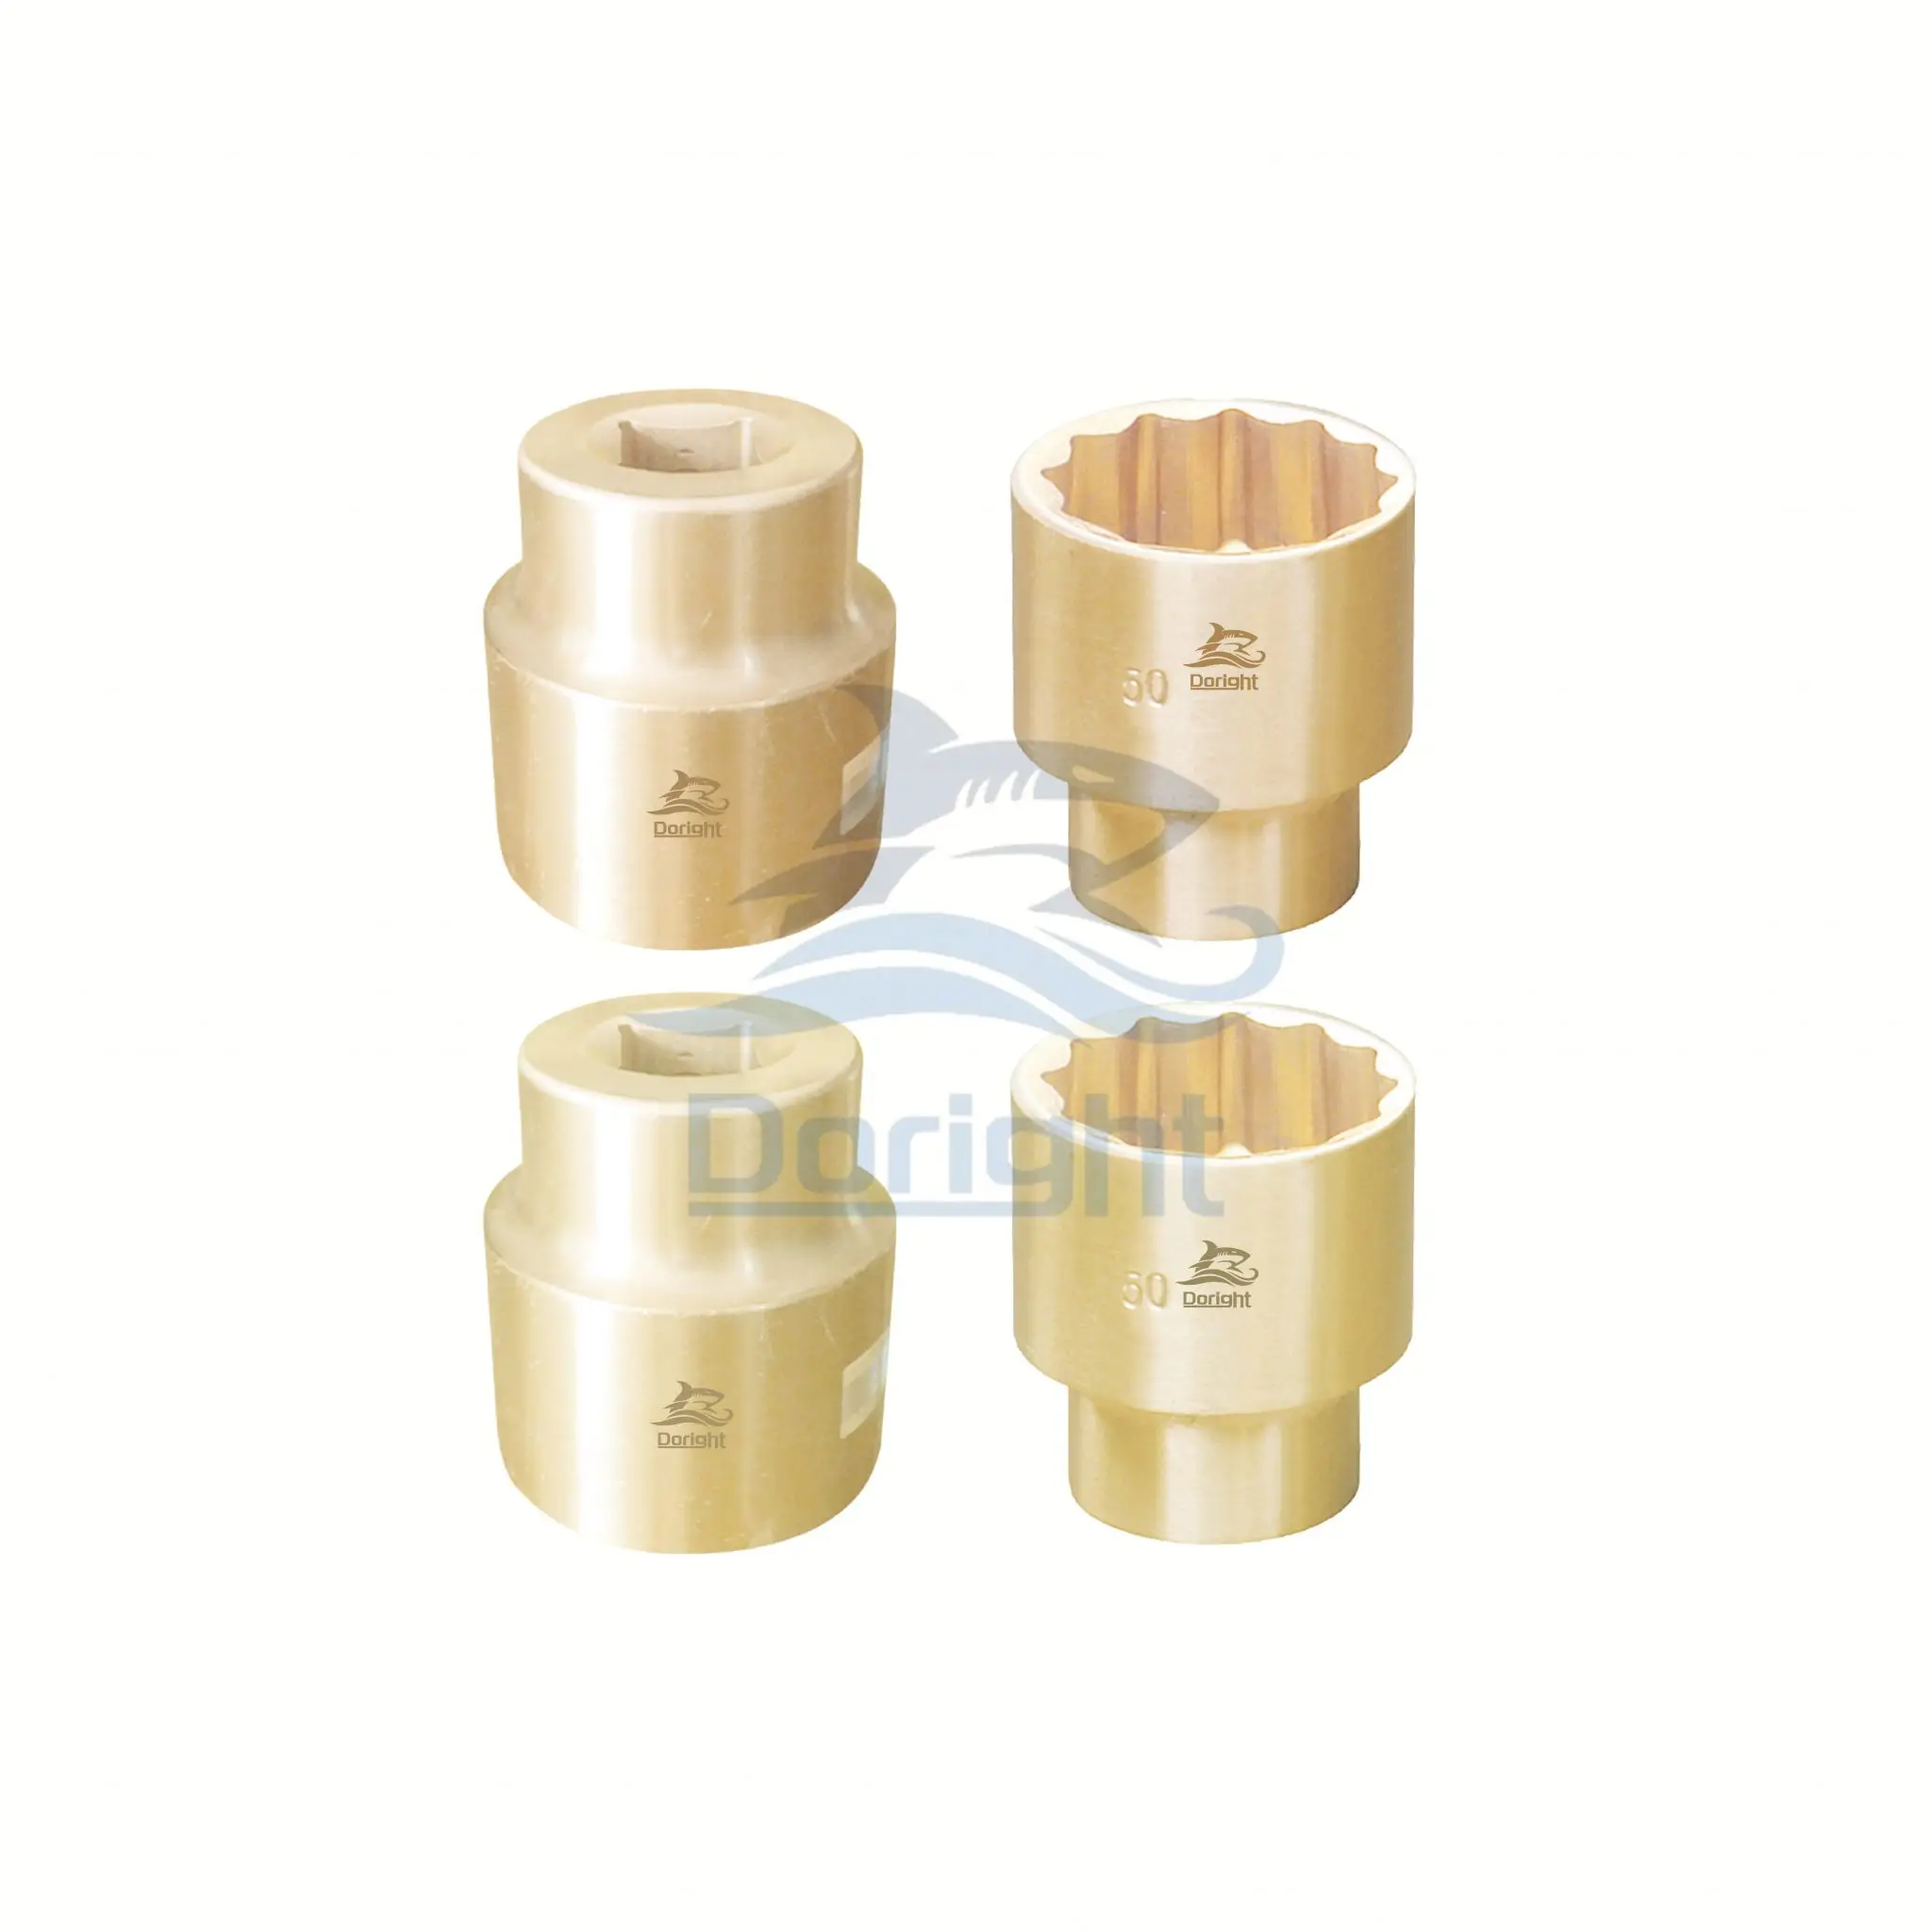
non sparking impact sockets are touted as the safe choice in flammable atmospheres, but I’ve learned the hard way that plugging them into existing workflows without thought creates new failure modes. First, compatibility — impact-rated, non-sparking alloys require different torque curves. When teams keep the same torque settings and power converters on their impact drivers, fasteners get under- or over-torqued. That leads to leaks or stripped heads later. Second, maintenance blind spots: corrosion-resistant alloys behave differently in repeated thermal cycles and in salt-heavy environments. We misinterpret wear patterns and let tools run longer than they should. I’m not saying the tools are bad — far from it. But in practice, a safe socket plus the wrong driver, the wrong torque program, or lax inspection equals a false sense of safety. Look, it’s simpler than you think: pair the right socket with proper torque control, validate against your hazardous area classification, and train crews on the small differences. We automated checks in one site (simple scripts that log torque profiles) and caught a dozen bad installs in the first month.
What’s the real risk?
The real risk is human complacency mixed with invisible technical mismatch. You can have ATEX‑grade sockets and still create ignition paths if the system-level parameters aren’t aligned. We must treat tools like nodes in a distributed system — edge components that need versioned configs and health checks, not one-off procurements.
Part 3 — Looking forward: principles, choices, and three metrics I trust
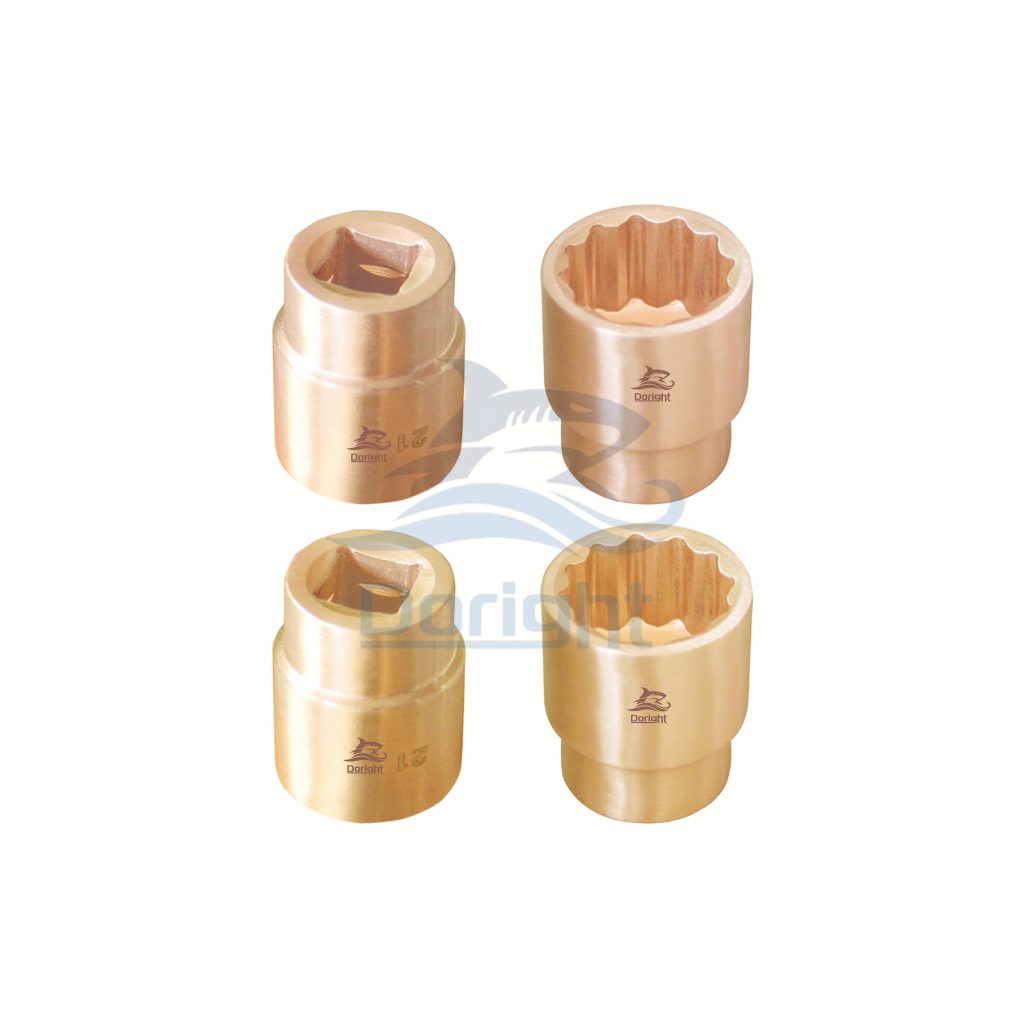
From here I move to the practical principles that have helped my teams avoid surprises. First: treat non-sparking socket heads as instruments, not consumables — they need calibration and environment-aware maintenance. Second: introduce simple automation (yes, more scripts) to capture torque signatures and maintenance logs so you can spot drift early — funny how that works, right? Third: test combos under real conditions before full rollout; a bench test in clean air doesn’t cut it. In this step I deliberately pair the physical tool with software checks and human-run spot audits. That mix reduced rework and unscheduled downtime on one site by measurable amounts within three months. I recommend evaluating solutions on three core metrics (more on those below). Meanwhile, I’ve linked the heads we actually put through that workflow — non-sparking socket heads — and the results were telling: fewer misthreads, fewer retrofit jobs, and clearer inspection records. — and yes, teams feel more confident when they can see the data.
What to measure
Here are three evaluation metrics I use when choosing and deploying non-sparking sockets: 1) Torque fidelity: measure variance from target torque under real load. Low variance means fewer leaks and failures. 2) Material lifecycle in environment: track corrosion and microscopic wear against expected cycles (salt spray, vapor exposure). 3) Integration overhead: time and effort to calibrate drivers, add logging, and train crews. If a product adds too much overhead, adoption stalls. I’ll be blunt: we pick tools that make audits easier, not harder. That keeps teams honest and managers asleep at night — in a good way.
In closing, I’ve seen the small changes that matter. Tighten your tool‑driver pairings, automate the boring checks, and treat sockets like part of your control plane. We focus on practical, measurable steps: torque control, corrosion checks, and integration effort. Those three metrics will tell you whether a solution will survive daily use or become shelfware. If you want a starting point for tested options, check the selection at Doright. I’m happy to walk through an example setup with your team — we’ve done it, and it works.






