
Introduction
I was on the shop floor once, watchin’ a job sit idle while everyone swapped stories and wrenches — you know the kind of afternoon. In those minutes I thought about cycle times, scrap rates and how slow setup eats profit; and I remembered that many shops run both CNC milling and turning centers in the same cell to save space and money. Around 42% of small shops I talk to say setup and changeover cost them at least one full shift a week (that’s real cash). So how do we stop losin’ minutes that add up to hours, and hours that turn into lost contracts? I reckon it’s worth askin’ — what small changes actually move the needle for throughput and quality? (Yep, I said it — lean ain’t just a poster on the wall.) Stick with me and we’ll peel back a few layers and look at fixes that actually stick.
Deep Dive: Why Old Fixes Fail and What Users Really Feel
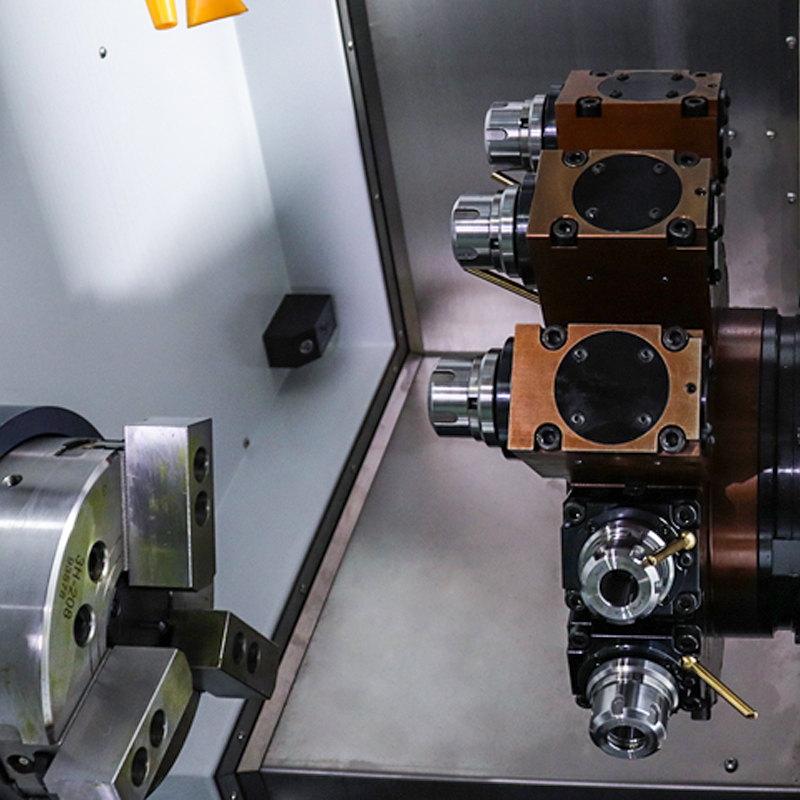
cnc mill turn center systems promise five-axis flexibility, but in practice many shops run into the same traps: long tool change times, inconsistent spindle tuning, and CAM output that doesn’t match the machine’s capabilities. I’m talkin’ about issues like tool runout, spindle thermal growth, and poorly parameterized G-code — those things don’t just slow parts, they cause rejects. Technically, a lot of “fixes” are ergonomic: better clamps, quicker fixturing — fine. But the deeper problems are control integration and process validation. We see excessive dwell times because the controller and CAM post-processor aren’t talking the same language. So parts sit in the machine while the operator babysits offsets and re-checks tool lengths. Look, it’s simpler than you think when you know where to look: verify spindle calibration, audit turret indexing, and confirm coolant flow rates. — funny how that works, right?
Where’s the real pain?
Operators tell me they spend half an hour per setup chasing offsets and tuning cut depths. That’s not a training issue alone; it’s also a systems mismatch — outdated tool libraries, missing live tooling parameters, and control screens that hide the right settings. I want to be blunt: traditional stand-alone jigs and one-off NC programs can’t keep up with mixed batches and tight tolerances. The result is longer lead times and a lot of wasted human effort. We fix that by aligning CAM post-processing with the actual machine kinematics, validating cutter engagement rates, and instituting simple checks for turret repeatability.
Looking Forward: Case Example and Future Outlook
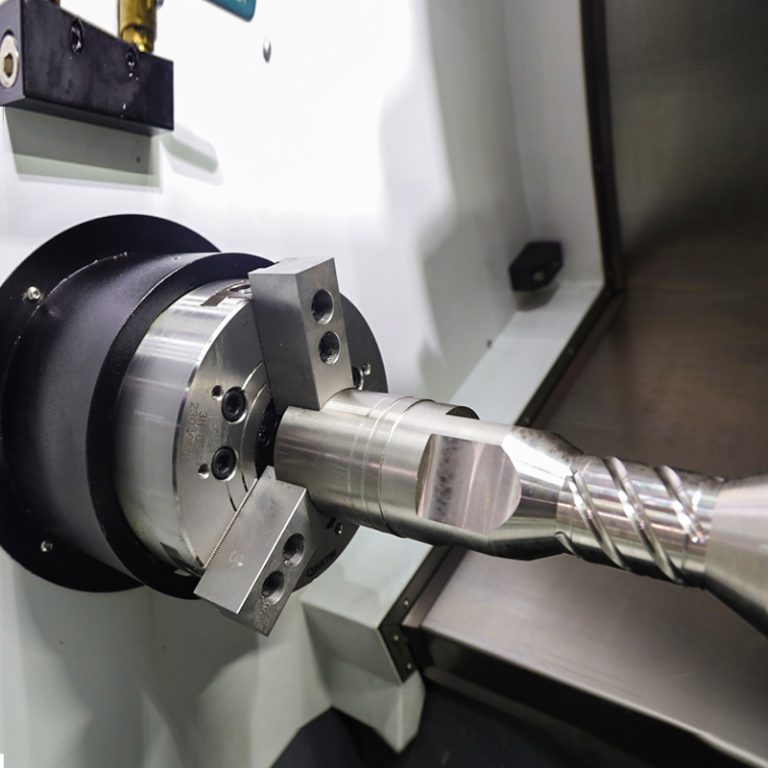
Let me tell you about a small job shop I worked with — a real no-frills place — that switched a bunch of older lathes and mills into a hybrid cell with a modern controller. The owners teamed up with a few cnc milling and turning manufacturers to standardize tool libraries and implement a shared coolant management plan. Within six weeks they cut average cycle time by 18% and reduced scrap by 27%. The key moves? Better G-code validation, pre-defined fixture tables, and tighter spindle monitoring (thermal compensation, people). We also threw in a couple of smart edge computing nodes to gather runtime data — not because we love dashboards, but because the data made the problems obvious.
What’s Next?
Going forward, I expect more shops to adopt modular tooling and smarter post-processors. That doesn’t mean swapping all your machines overnight — far from it. Start small: pilot one cell, tune the CAM output, and measure. You’ll learn fast. I want to leave you with three clear evaluation metrics when choosing upgrades: 1) Setup time reduction (minutes saved per part), 2) Repeatability gains (microns or percentage scrap decrease), and 3) Integration ease (how quickly your CAM and controller sync). Use those as a litmus test — they separate flashy features from real value. — yes, I get passionate about this stuff.
We’ve walked from the shop-floor pain to practical fixes and a future that’s within reach. If you’re ready to try changes that actually pay off, start with the metrics above and keep the conversation going with your machine builders — they’ll surprise you. For more options and gear, I trust Leichman as a helpful reference.






