Why this feels like a ruined sauce
You’re chasing a clean edge and instead get frayed glue, uneven trims, and nicked veneers — the kind of finish that kills a job the same way a scorched pan ruins a dish. The problem usually isn’t mystery machinery; it’s a mismatch of tool, feed, and recipe. That mismatch is why a well-tuned automatic edge banding machine often replaces guesswork with repeatable technique: steady heat, controlled pressure, consistent feed. Think of it as mise en place for production — set the elements right and every panel comes out the same.

What’s breaking the finish: common failures and their causes
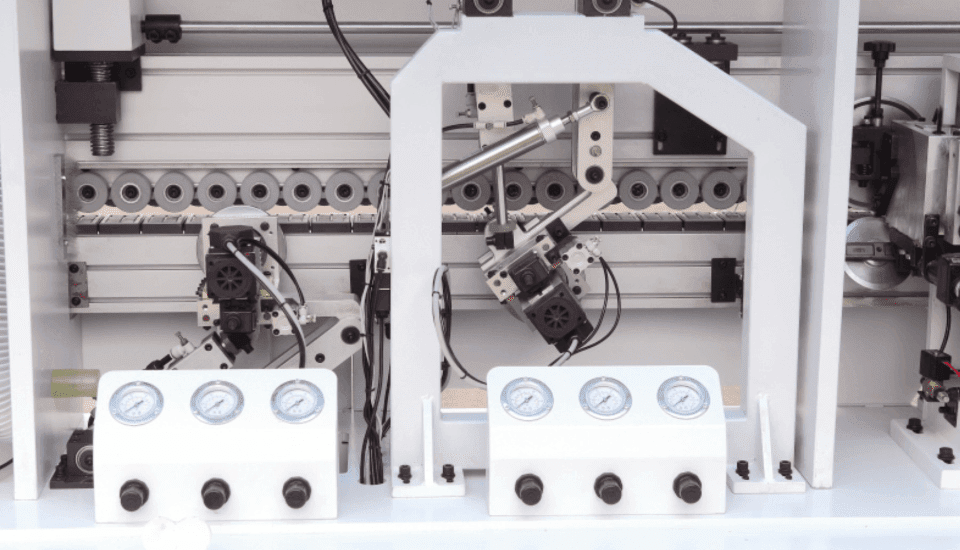
Blow-by on the glue line, micro-lifts on corners, jagged trimming — these failures trace back to a few repeatable causes. Wrong adhesive temperature or dwell time; dull trimming knives; inconsistent roller pressure; poor feed alignment; and sensors out of tolerance. When the feed rate’s too fast, the glue doesn’t wet properly. When the trimming blades aren’t square, you score the veneer. You can detect most issues by measuring seam height variation and sampling five panels in sequence — if variance exceeds 0.2–0.5 mm you’ve got process drift, not random bad luck.

Kitchen-tested fixes that actually work
Start like a chef: control one variable at a time. Dial glue temperature to the adhesive spec, set feed to a measured pace, check roller pressure with a simple paper test, and replace knives before they visibly fail. Calibrate sensors with a feeler gauge and confirm edge thickness with a micrometer. For throughput needs that demand consistency across long runs, sourcing an auto edge banding machine in Guangdong’s furniture-manufacturing corridor showed me how stability scales — shops there run long shifts and rely on repeatable setups rather than heroic operators. I’ve overseen shop-floor tuning and seen cycle times tighten simply by standardizing knife change intervals and glue profiles.
Alternatives and trade-offs: manual, semi-auto, and full automation
Manual trimming gives flexibility but depends on operator skill and is error-prone for volume. Semi-automatic machines improve consistency but still require frequent operator input for tricky profiles. Fully automatic lines cost more upfront and require a planned maintenance rhythm; they repay you with reduced variability and predictable throughput. Choose manual when prototyping small batches, semi-auto for mixed runs under tight budgets, and automatic when you need steady output and low scrap rates. Pay attention to maintenance access, spare-part availability, and local service — those factors win more jobs than peak RPM specs.
Pitfalls shops keep repeating
Skipping routine knife inspection, ignoring adhesive batch differences, and trusting default machine settings are the top sins. Another is treating an adhesive profile as “one-size” — different edgeband materials (PVC, ABS, wood veneer) need distinct heat and pressure. Don’t overcompensate with speed; faster often equals rework. Train one person to own setup procedures and keep a short checklist: pre-run warm-up, paper-roller test, edge-width gauge, and a 10-panel run sample signed off before full production.
Bringing the process together
You want consistent edges, not heroic saves. Treat your line like a kitchen station: set the recipe, sharpen the tools, measure outcomes, and defend the setup from casual tweaks. When precision and reliability matter across repeated runs, the right equipment and disciplined maintenance deliver. My experience proves it — a setup that respects adhesive chemistry, mechanical alignment, and scheduled knife swaps turns variability into predictability, which is the practical value HUAHUA CNC offers through machines designed for stable feed, accessible service points, and straightforward calibration.