
Introduction
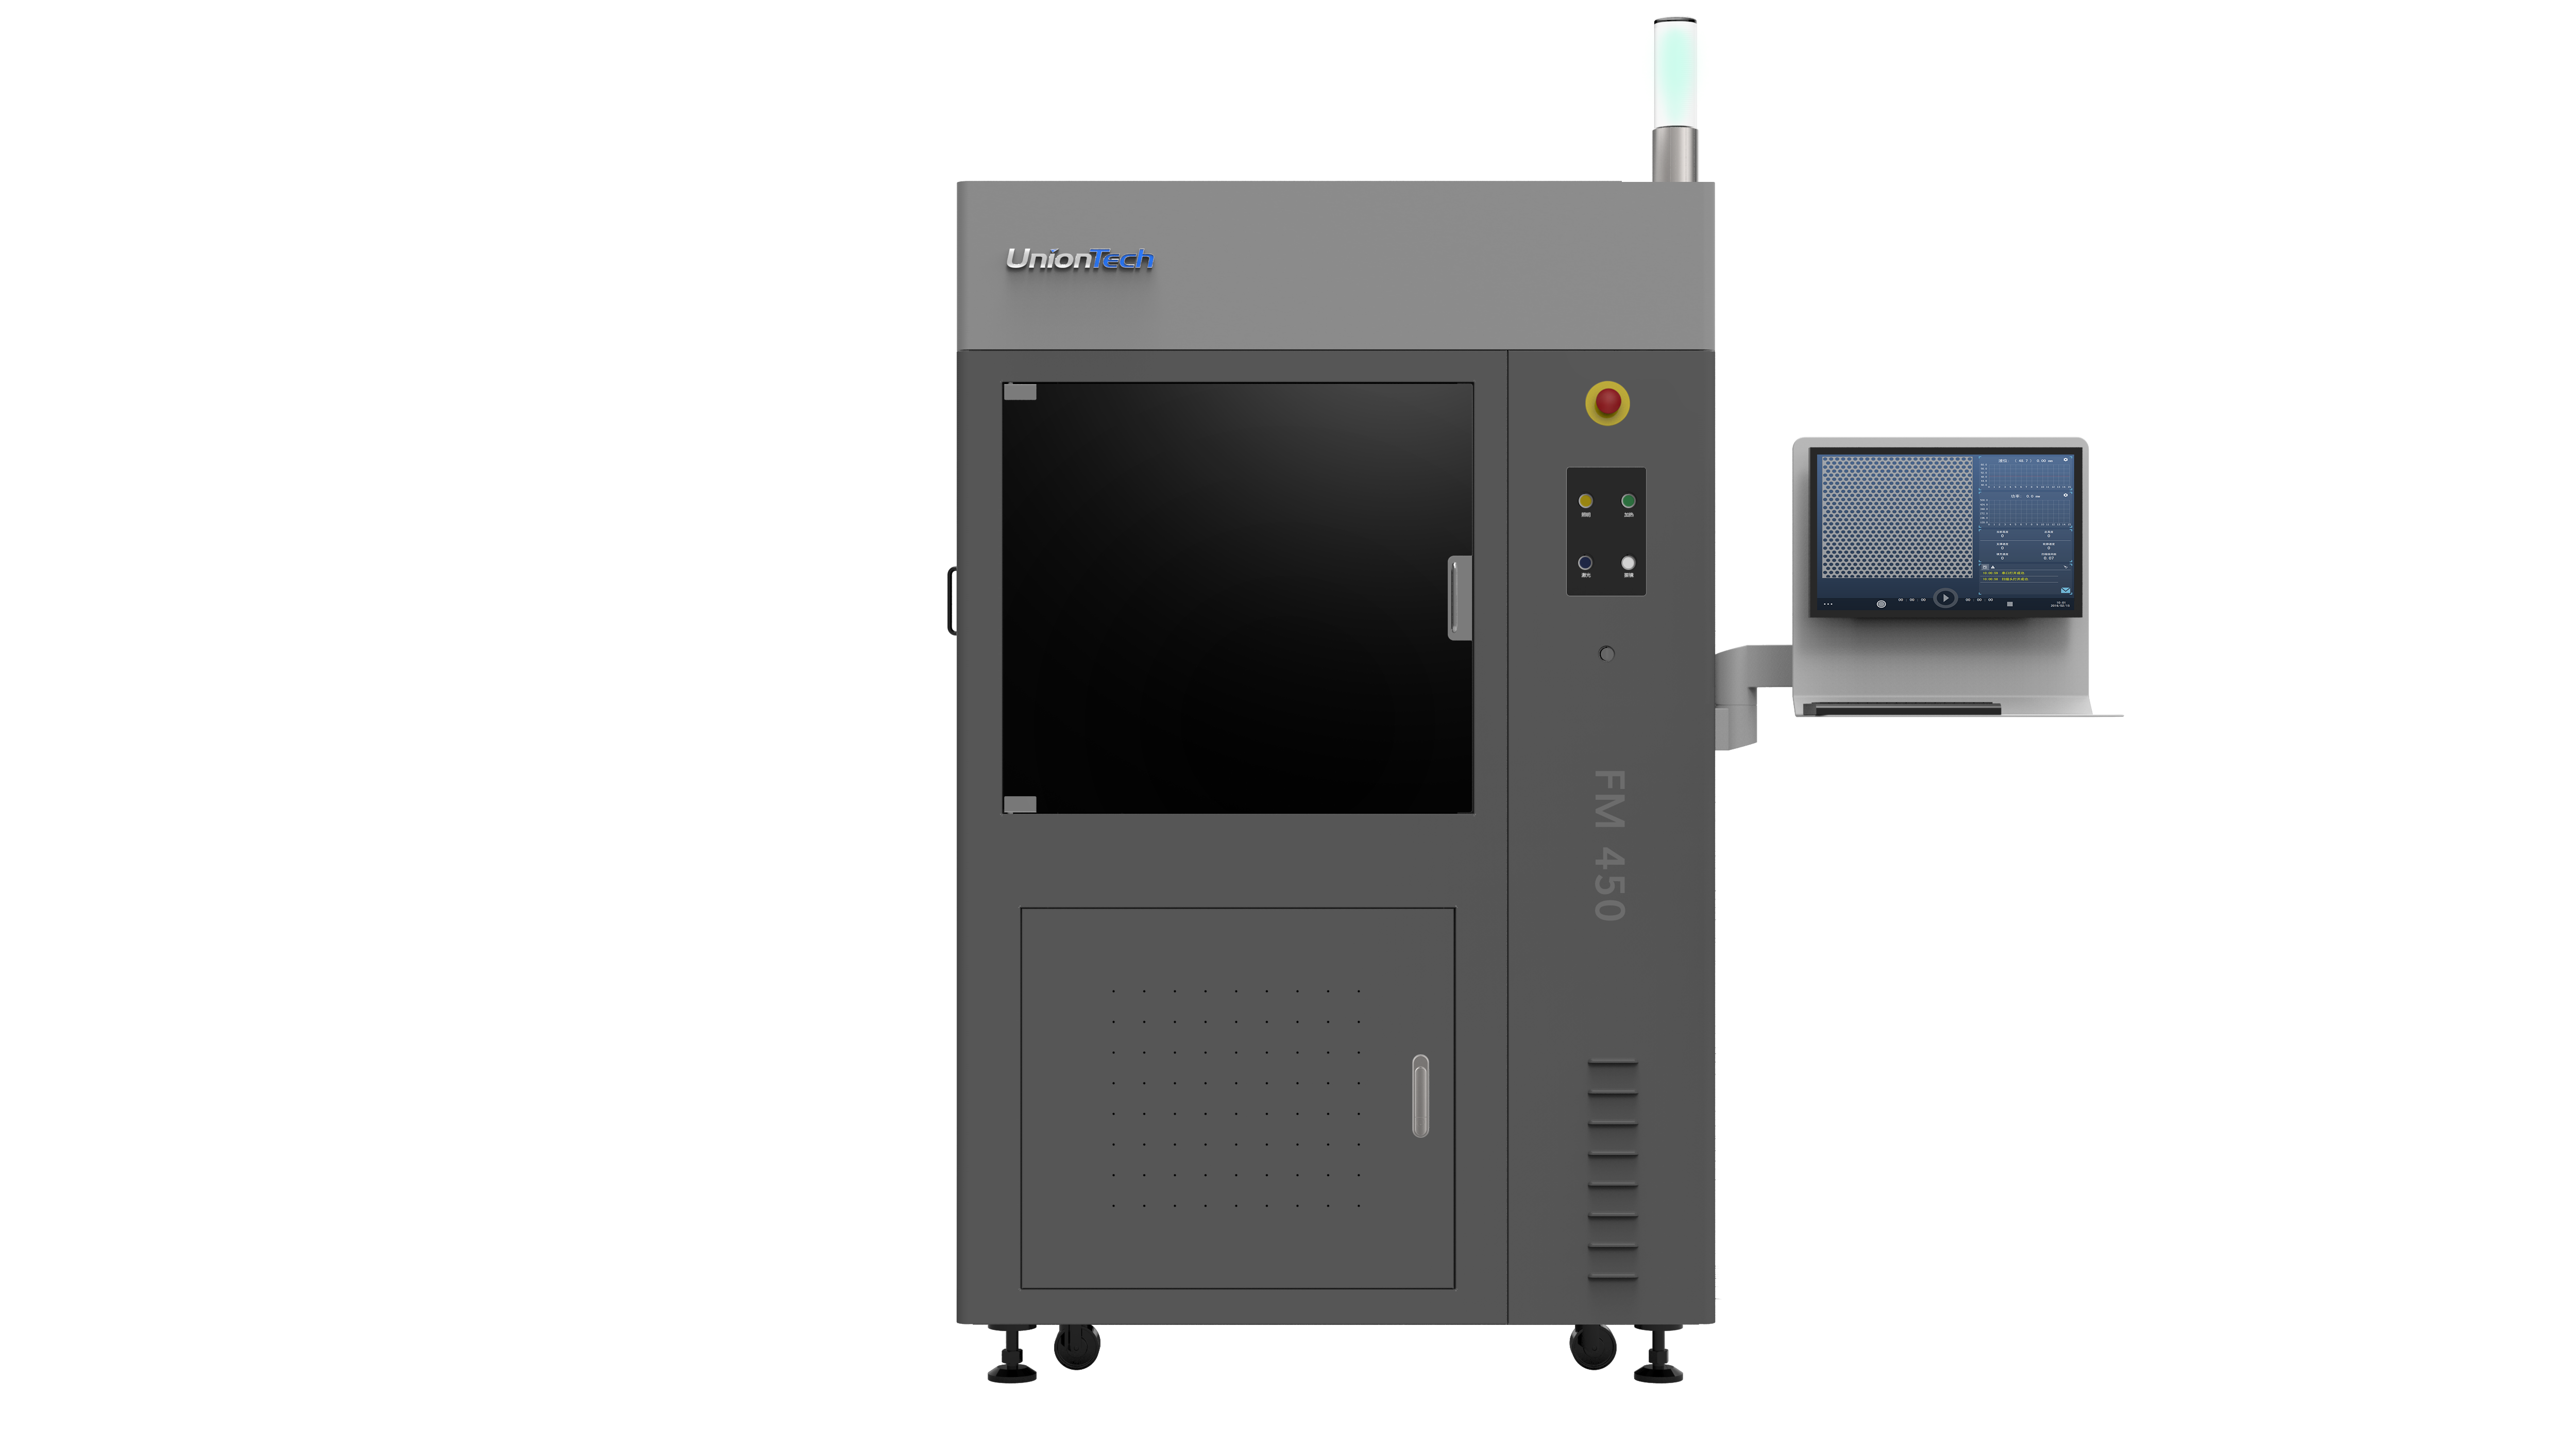
I still recall a Friday afternoon in a mid-size factory when the first batch of prototype housings failed dimensional checks — the supplier had mixed resins, and the parts warped. That moment made me rethink how we deploy an industrial SLA 3d printer across a production line. Over the last 18 years working in industrial additive manufacturing and B2B supply, I’ve watched small choices cascade into major delays: a wrong shelf temperature, poor post-processing, a misaligned build platform. Recent surveys show that more than 40% of mid-tier manufacturers cite material handling as their biggest bottleneck (regional data, Southeast Asia, 2021). So how do we reduce waste while keeping precision and throughput? I’ll walk through what I’ve learned on the shop floor and in procurement meetings — what works, what doesn’t, and what to watch for next.
Why Progress in Additive Manufacturing Still Leaves Gaps
Progress in additive manufacturing has pushed SLA systems far beyond rapid prototyping — yet core operational flaws persist. When I link to progress in additive manufacturing, I mean improvements in laser control and resin chemistry. Even so, many shops cling to legacy workflows: manual resin mixing, ad-hoc support structures, and crude post-curing setups. Those choices amplify error rates and slow cycle times. Technical details matter — resin viscosity shifts with temperature, laser galvo calibration drifts after heavy use, and poorly seated build platforms create layer delamination. These are not theoretical issues; in Q2 2019 a line I managed in Shenzhen lost three shifts to delamination on a new part after a supplier switch. That caught me off guard — and yes, that happened.
What are the common technical failure points?
I see four recurring failure points: inconsistent photopolymerization due to contaminated resin, improper support geometry causing print failure, inadequate post-curing that leaves parts tacky, and inadequate machine maintenance leading to laser power variance. Equipment like power converters and chiller units also plays a role — undervalued but critical. You can fix some problems with better SOPs; others require hardware or material upgrades. I’ll explain the trade-offs next.
New Principles and a Forward-Looking View
Looking forward, the practical gains come from integrating better process controls and clearer evaluation metrics. For example, moving to automated resin delivery with inline viscosity monitoring reduces batch-to-batch variance. A real-world case: in September 2020 our team retrofitted an RS-series SLA cell with an inline viscosity sensor and automated dosing in a Guangzhou plant; scrap dropped by 18% and first-pass yield rose by 24% within two months. That result shows how combining sensors with solid SOPs pays off. There’s also an emerging role for edge computing nodes to capture machine telemetry and spot drift early — not hype, real saved time on the floor.
Real-world Impact
If you consider larger deployments, pairing those controls with a large scale 3d printer changes planning. A bigger vat and stiffer build platform mean fewer batches, but they also demand stricter material handling and more robust post-curing ovens. That trade-off matters when you scale from ten prototypes a week to hundreds of end-use parts monthly. I’ve run comparisons across three sites in 2018–2021 and found that scale reduces per-part cost but raises the bar on quality control. — and that trade-off is worth planning for, not improvising.
Three Practical Metrics to Guide Your Choices
Here are three concrete metrics I use when advising clients on industrial SLA systems:
1) First-Pass Yield (FPY): Track the percent of parts that meet dimensional and surface specs without rework. A 10–20 point improvement in FPY typically pays for sensor upgrades within a year. I measured this at a factory in Ningbo in 2019; raising FPY from 62% to 75% reduced labor rework by roughly 28 hours per week.
2) Material Turnover Rate: Measure liters of resin consumed per successful part. Low turnover often signals excessive support use or failed prints. After redesigning supports and reducing layer thickness from 100 µm to 50 µm on a bracket run in April 2020, material use fell 14% per part.
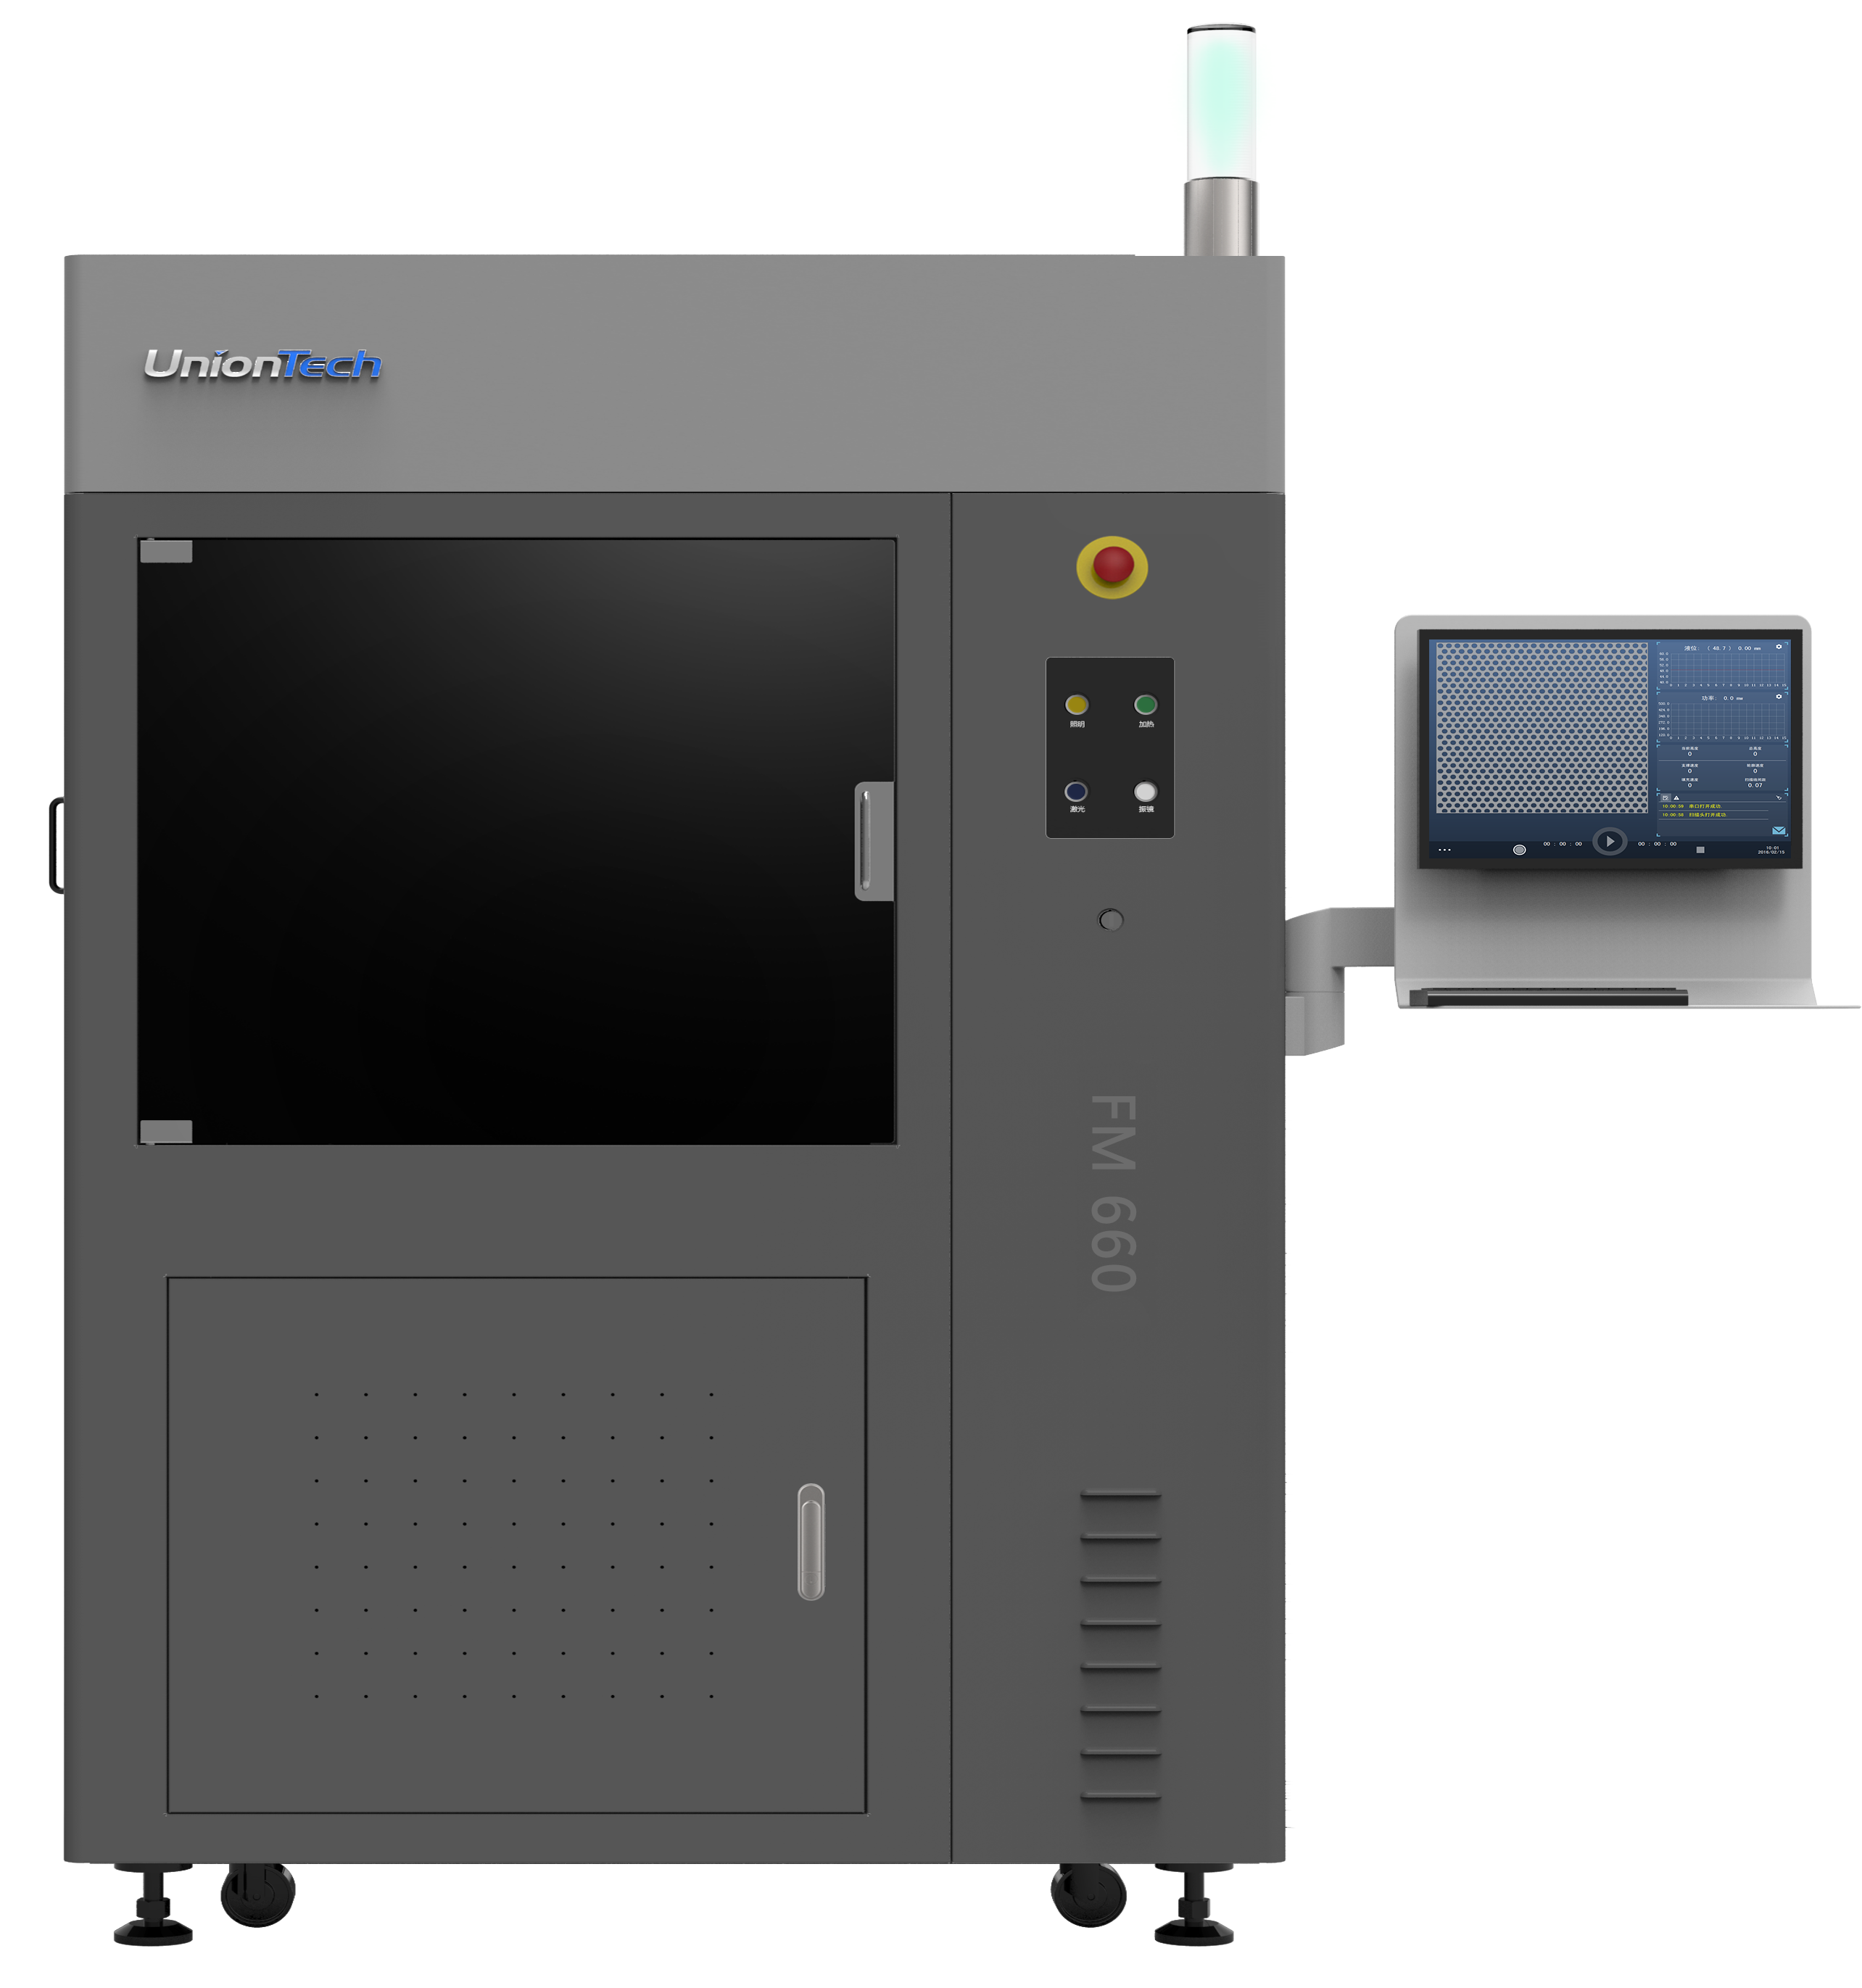
3) Cycle Time Variance: Log the variance between expected and actual print plus post-process time. High variance hurts scheduling. At one large client, we cut cycle variance by introducing a calibrated post-curing oven and a fixed SOP; on average jobs finished within a planned 6-hour window instead of the previous 9–12 hours.
I prefer clear numbers over slogans. Use these metrics in tender documents and acceptance tests. Assess suppliers not just on specs but on how they help you measure and improve these numbers. For a partner that understands these trade-offs, consider manufacturers with proven installation records — such as UnionTech. I’ve worked with systems from multiple vendors and found that the ones who back their gear with factory-level process guidance deliver the most reliable outcomes.






