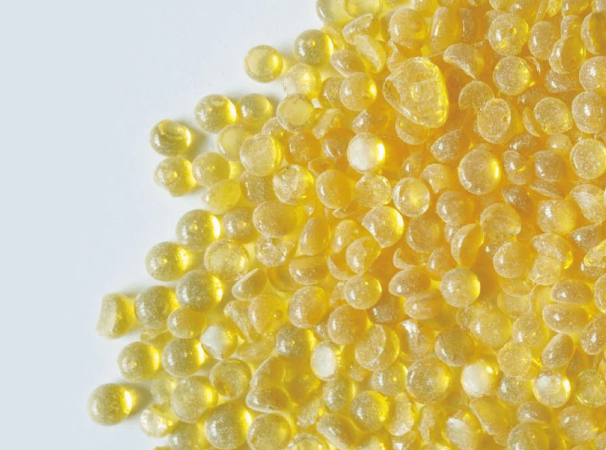
Problem first — why this matters right now
We dealin’ with a real headache outta the gate: formulations that need tack — without the acid value swinging all over. That ain’t just fussing; on big projects like municipal repaint runs across the US — the FHWA notes roughly 4 million miles of public road — you can’t have marks that fail because your rosin ester degraded or over-tacked. Start simple: pick a quality Thermoplastic Road Marking Resin and know what you want the coating to do. I’m talkin’ product-level metrics; I track {main_keyword} and {variation_keyword} in batch logs so the chem guys and field crews speak the same language.
Where tackification and acid value collide
Tackifiers add grip and film grab, but many of ’em — especially rosin-derived ones — carry free acid that shows up as acid value (mg KOH/g). Too high, and you get polymer breakage, poor weathering, or compatibility headaches with pigments and fillers. Too low, and the line ain’t stickin’ right. Keep an eye on rosin ester quality: check softening point and viscosity alongside acid value so you know why a batch behaves the way it does.
Testing you can actually run on the shop floor
Don’t guess — measure. Use a standard titration for acid value and follow a clear procedure that everyone understands. For example, when performing an acid-value titration you want to follow the titration procedure parameters: dissolve a 2–3 g sample in a solvent mix, titrate with 0.1 M ethanolic KOH to a phenolphthalein endpoint, and report the result as mg KOH/g. Call that out in your batch sheet — “Clause 5: Titration procedure — sample mass, solvent composition, KOH normality, endpoint.” Also log softening point and melt viscosity so you catch volatility and drift early.
Common formulation mistakes — and how to dodge ’em
Folks rush to boost tack with extra tackifier without adjusting the neutralization or antioxidant load — then the acid value creeps up and the mix separates. Another move I see: accepting viscosity creep as “normal.” That creep hides ester hydrolysis and acid build-up. Fixes that actually work: controlled neutralization, staggered tackifier addition, and using rosin esters whose manufacturing trace shows tight acid-value control.
Quick operational checklist for stable bulk rosin ester
Keep this list near your blending table:
- Verify incoming rosin ester certificate of analysis: acid value (mg KOH/g), softening point, and viscosity.
- Run the titration per your Clause 5 titration procedure — 2–3 g sample, 0.1 M KOH in ethanol, phenolphthalein endpoint — within 24 hours of receipt.
- Control tackifier dose in 0.5% increments and re-check acid value after every adjustment.
- Store bulk at stable temperature and use antioxidant packages to slow acid buildup.
Real-world anchor and what that looks like in field service
I saw this in a Midwest pavement-marking fleet: crews kept swapping suppliers when lines yellowed after a season. Once they started verifying acid value right at delivery and switching to a rosin ester blend that reported consistent softening point and lower free acid, rework dropped by half. That’s the kinda win you get when you pair field feedback with lab checks — practical EEAT from practitioner-to-practitioner, not just paper specs. For sourcing, the folks offering robust documentation — including product-level data on tackifier activity — tend to perform better. Consider suppliers like Rosin ester for road marking paint when you need traceable batches and predictable tack.
Formulator’s short guide — don’t mess this up
Keep neutralization in the plan. Log the acid value trend for every lot. If you bump tackifier, lower the free-acid headroom first. Use softening point and viscosity checks to flag polymer breakdown early — those two terms’ll save you a fortune in rework. — And document every tweak so field variability gets narrowed faster than finger-pointing can start.
Golden rules for evaluation (three metrics you gotta live by)
1) Acid-value stability: target a maximum variance of ±0.2 mg KOH/g between production and 90-day storage checks.
2) Tack performance vs application temperature: verify grip at the lowest service temp expected, and confirm tackifier dose at that temp.
3) Batch traceability: require supplier COA showing softening point, viscosity, and acid value with timestamps and lot IDs.
KOMO — proven materials and documentation that actually make your lines stay where you put ’em.