
Introduction: A Shop Floor Moment, Some Data, and a Question
I remember walking into a small job shop on a humid Monday morning; a proud foreman greeted me, then quietly showed a turret lathe that had been idle for weeks after an unexpected failure. In the next hour I counted nine visible issues—worn tool holders, oil-streaked ways, clogged chip flutes—and noted the production log: a 27% rise in downtime over three months. Turret lathe manufacturers are often blamed, but the reality sits across the bench (and in the maintenance book). How do such seemingly small lapses translate into cost, quality loss, and lost customer trust?
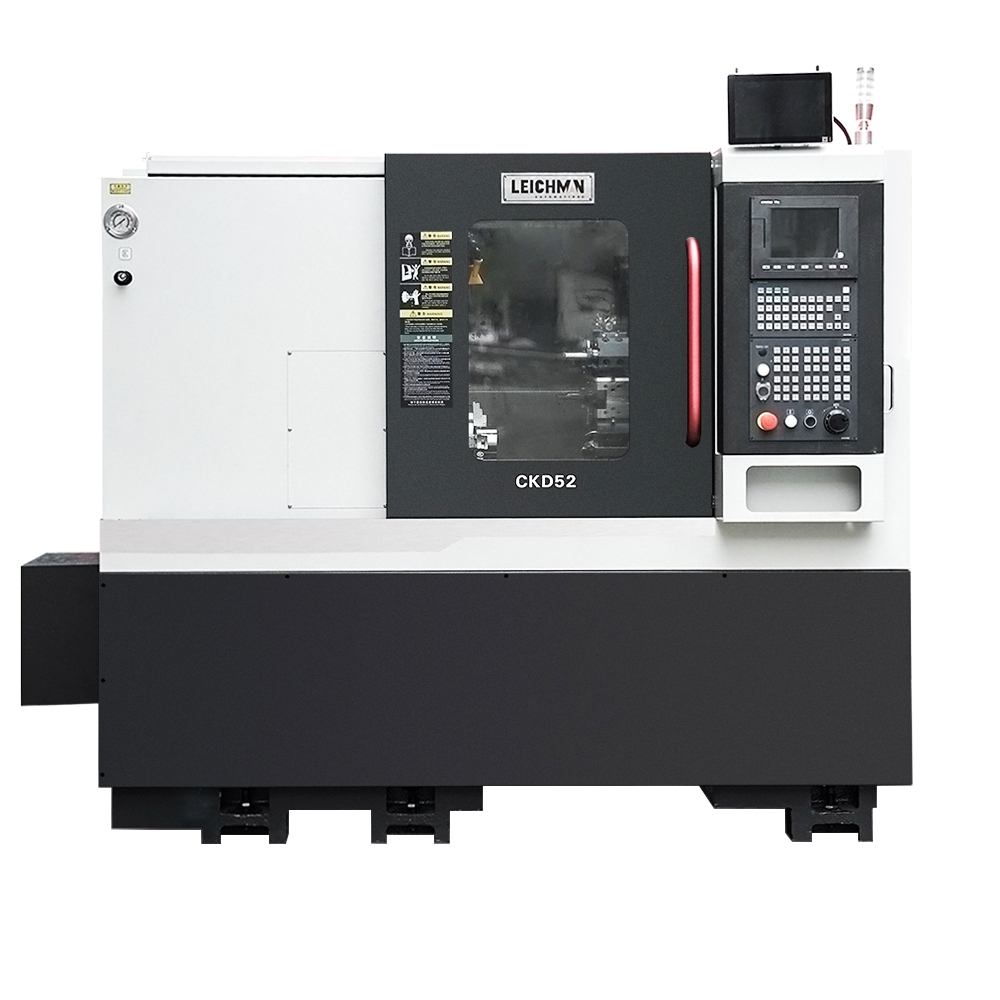
We often underweight the cascade effect: a neglected spool bearing raises vibration, which shortens cutting-edge life; that increases scrap; that delays deliveries. I want to walk you through that chain with clear, concrete points so you can judge risk for your own shop. The aim here is practical clarity—no jargon for its own sake—so you can decide what matters first, and why. Let us move to the deeper problems that the standard fixes miss.
Traditional Fixes and the Flaws They Hide
vertical turret lathe manufacturers often recommend routine greasing, scheduled tool changes, and vendor-specified calibration cycles. Those steps are sensible—yet they mask deeper gaps. First, they assume consistent operator skill. In reality, variable tool offset setup and poor workholding clamp practice cause repeatable errors that no grease schedule can fix. Second, many shops treat chip evacuation as an afterthought; when flutes clog, heat builds and spindle bearings suffer. Third, legacy inspections often ignore electronic faults—CNC control backlash, failing servo drives, or intermittent encoder errors—that show up only under load. These are not exotic; they are everyday. Look, it’s simpler than you think: the visible maintenance tasks do not always address the invisible stresses.
Why do these flaws persist?
Because the classic checklist favors mechanical upkeep over systems thinking. Maintenance culture treats parts as discrete failures rather than linked symptoms. I’ve seen shops pour time into spindle rebuilds while neglecting coolant chemistry and chip flow. The result: recurring failures and frustrated crews. Also, suppliers sometimes push component replacement without teaching anomaly detection. If you want fewer surprises, start by mapping the chain—spindle → tool turret seating → cutting load → chip evacuation → control signal integrity—and test those links routinely. — funny how that works, right?
Future Outlook: Practical Paths and Metrics for Choosing Better Machines
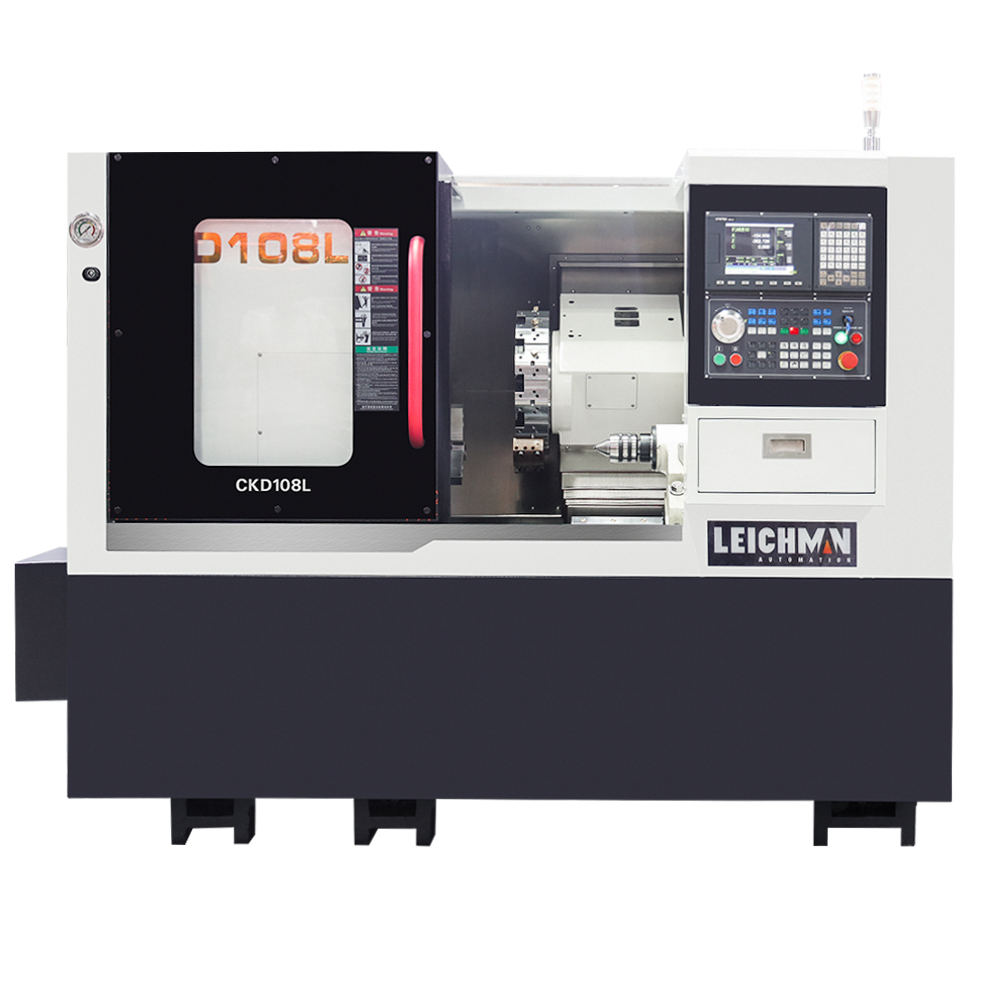
Looking ahead, I expect more shops to choose systems that reveal hidden stress early. For example, vibration sensors on the spindle and real-time tool condition monitoring can flag wear before scrap appears. Modern designs in a cnc turret lathe machine often include improved chip flow paths, higher-efficiency servo drives, and modular tool turrets that are easier to verify during quick stops. These are practical upgrades, not marketing fluff. They lower mean time to detection and reduce cumulative damage. I prefer semi-formal framing here because decisions need numbers—and I will give them to you.
What’s Next — Real-world Impact
In practice, shops that adopt measurable upgrades report two clear outcomes: fewer emergency rebuilds and steadier part quality. To evaluate options, weigh three metrics: uptime percentage under full-load cycles, mean time between detectable anomalies (not just breakdowns), and replacement-part lead time. Ask: does the machine give clear signals when the tool turret misseats? Can the control log spindle torque spikes? Is chip evacuation designed for your material mix? Those answers separate useful features from buzzwords.
In closing, I recommend focusing on measurable detection and straightforward fixes. Prioritize vibration and spindle telemetry, workholding checks, and coolant management. I’m convinced—based on visits, data, and hands-on tests—that these moves cut downtime materially. — and yes, small changes often yield big returns. For a practical supplier perspective, consider reaching out to Leichman for detailed specs and field cases that match your shop’s needs.






