
Introduction — a workshop, a number, and a question
I remember standing in a small shop, the tang of coolant in the air, watching an old lathe cough and then sing as it cut aluminium—howzit, those moments stick with you. CNC turn mill center manufacturers (many of them small to mid-sized) tell me roughly 60% of their shops still lose time to changeovers and setup snarls. That figure made me pause — if half your day vanishes in adjustments, what’s really holding you back?
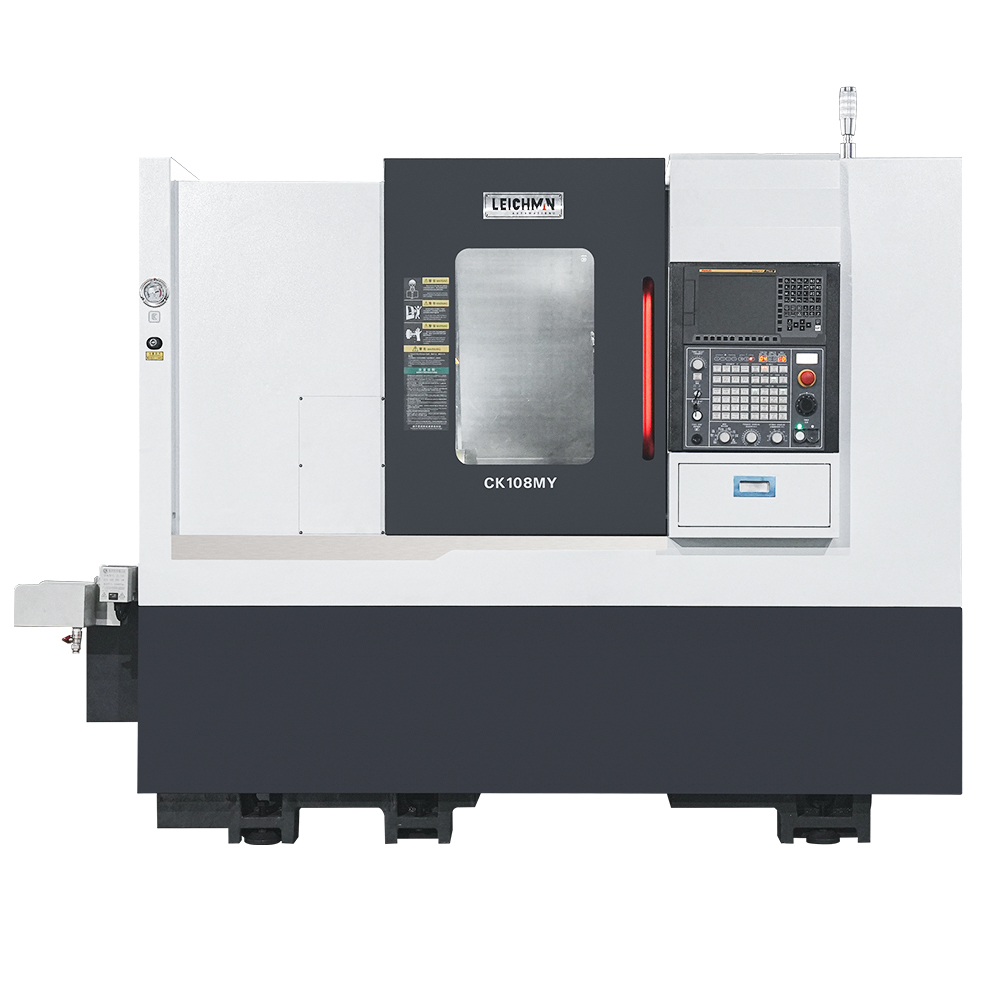
So let’s be plain: I want to share what I’ve seen, what works, and where the real headaches hide (eish, it’s not just the machine). I’ll talk about spindle speed choices, tool turret clashes, and why your servo motors alone won’t fix throughput. Ready? Let’s move into the guts of the problem and then forward to solutions.
Part 2 — Where the old fixes fail: deeper pains in cnc multi axis turning milling center operations
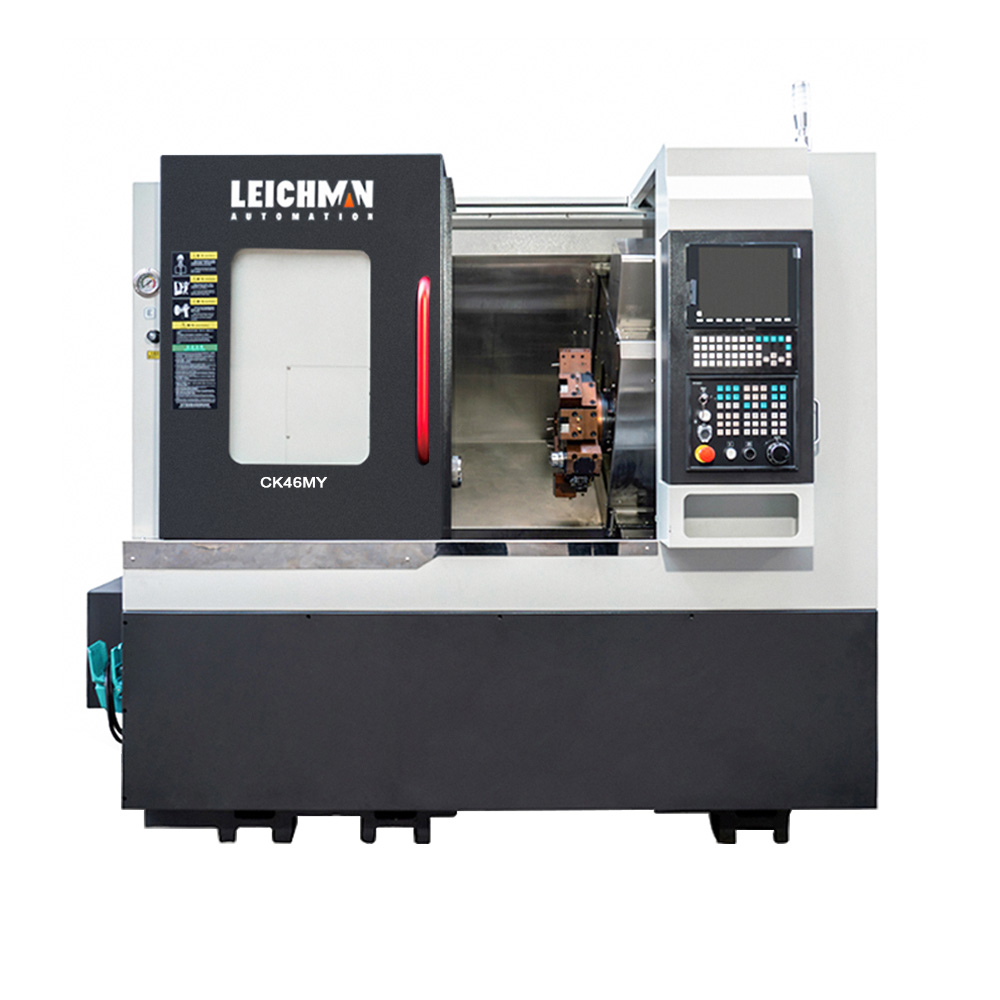
When we look at a cnc multi axis turning milling center, people assume adding more axes or a fancier controller cures all. In my experience that’s not the case. The traditional fixes—more tooling, faster spindle speeds, tighter tolerances—often expose other faults: poor tool management, weak CNC programming, and clumsy turret indexing. These create ripple effects. Shops swap parts faster but keep tripping over setup errors and scrap.
Look, it’s simpler than you think: if linear guides are dusty, precision goes out the window. If live tooling lacks rigidity, chatter sneaks in. I’ve seen power converters and control boards pushed to their limits because the workflow wasn’t changed—only the kit. You can buy axis redundancy, but if your workflow still routes parts the old way, cycle time won’t budge. In short, the “more hardware” band-aid misses the system problems. Why? Because the human and software side—tool offsets, fixture strategy, operator training—gets left behind.
Why does this keep happening?
Because people treat machines like magic boxes. They expect spindle speed to save them and forget basic setup planning. We need to stop that. — funny how that works, right?
Part 3 — Future outlook: practical next steps and how to judge new solutions
Looking ahead, I favour a combo approach: smarter software, clearer workflow, and measured hardware upgrades. For a workable future with a cnc mill turn center, think modular control logic, better sensor feedback (edge computing nodes can help), and standardised fixturing. These principles cut cycle time because they attack root causes—tooling chaos, poor programming habits, and inconsistent setup. We’ll need better CNC programming templates, consistent tool libraries, and a focus on spindle speed maps that match real cuts.
In real shops I work with, the shift starts small: standard work instructions, a simple checklist for turret indexing, and regular inspection of linear guides and bearings. Then the team layers in predictive monitoring and data from power converters or current sensing. The gains aren’t just faster runs; they’re fewer surprises and happier teams. — and yes, you’ll see uptime climb.
What’s Next?
Before you invest, here are three metrics I use to evaluate any change: 1) Net cycle-time reduction per part (real measured seconds); 2) First-pass yield improvement (less rework and scrap); 3) Total setup time saved per shift (minutes saved across jobs). If a proposed solution doesn’t move at least two of these, I’m sceptical. We’ve got to be practical. I want tools that help operators, not replace judgement. In the end, smart choices beat flashy specs.
I hope this reads like someone who’s been in the shop beside you—calling out what’s broken and pointing to fixes that scale. For gear, guidance, or windows into modern mill-turn solutions, check out Leichman.






