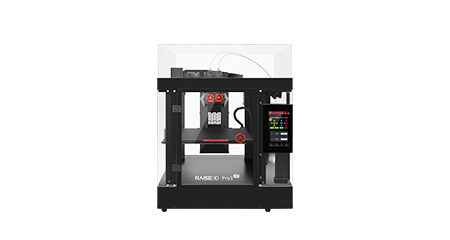
How Engineering Teams Tighten Layer Adhesion and Boost Tensile Strength with a High-End Raise3D Workflow
User-focused opening: what teams really need
Front-line engineering groups care about repeatable parts more than glossy specs. They want parts that bond reliably and hold up under load, not just pretty prints. Start by centralizing slicer profiles and toolchains—team members should share a single, tuned 3d printer slicer profile so settings don’t drift between operators. That one move cuts variance and speeds up root-cause work when a batch shows poor layer adhesion or inconsistent tensile strength.
Practical variables that move the needle
The core levers are simple: nozzle temperature, print speed, extrusion multiplier, and part orientation. Raise3D Pro2 Plus users often find small temp tweaks and a tighter extrusion multiplier produce big gains. Use moderate print speed and raise nozzle temperature a hair within the filament’s recommended range to improve inter-layer diffusion. Orientation matters too—align the primary load vector with continuous filament paths to raise tensile strength without adding mass.
Operational production teardown: profiles and common mistakes
Teams routinely stumble on a few repeat offenders: inconsistent bed leveling, overly aggressive cooling, and relying on default support patterns. When you perform an operational production teardown, tune the {main_keyword} settings per filament and document them. For resin or SLA-like needs, adjust the {variation_keyword} to control layer cure overlap and avoid exaggerated supports. Don’t skip a simple visual inspection of first-layer extrusion—small errors there echo through the whole print.
Tactical checklist that saves time on the floor
Adopt a short, reproducible checklist for each run. Typical items include: proper bed leveling and adhesion prep, confirmed nozzle and bed temps, calibrated extrusion multiplier, and verified filament diameter. Keep one lab notebook or digital log per machine so you can trace a bad part back to a profile change. Small discipline here beats large troubleshooting sessions later.
Real-world anchor and hands-on note
I spent a week with a Detroit automotive prototyping shop refining their Raise3D Pro2 Plus workflow; they cut failed tensile tests by half after standardizing profiles and controlling print orientation. That practical result matches broader industry observations—additive manufacturing teams that log settings and enforce a single slicer baseline reduce variation significantly. For resin-based parts, teams should also evaluate a dedicated resin printer slicer workflow focused on layer cure and support geometry to protect fine features.
Common mistakes and simple fixes
Many groups overcomplicate cooling. Too much fan right after extrusion prevents layer melding; dial back cooling on critical load-bearing surfaces. Another frequent misstep is over-relying on thick shells instead of changing infill strategy or raster orientation—sometimes a different raster angle with a well-tuned extrusion multiplier is the smarter path. Finally, avoid swapping filament brands without revalidating profiles—diameter and melt behavior vary enough to ruin a print.
Measurement and validation—what to track
Measure three things consistently: tensile strength (standardized test coupon), interlayer adhesion (peel or lap test), and dimensional fidelity. Use the same test geometry and testing speed so results are comparable. Record nozzle temp, bed temp, print speed, extrusion multiplier, and orientation with each test. That dataset makes optimization decisions factual instead of opinionated.
Three golden rules for teams (Advisory)
1) Lock a canonical slicer profile for production machines and only change it via a documented change request; this prevents drift. 2) Validate every filament with small test coupons for tensile strength, then scale to functional parts—don’t assume one filament equals another. 3) Prioritize orientation and extrusion tuning before adding bulk material; correct raster and extrusion multiplier choices typically beat heavier shells for strength and weight.
When teams apply disciplined profiles, consistent testing, and sensible orientation choices, the Raise3D Pro2 Plus becomes a reliable production resource rather than a bench experiment—Raise3D. –